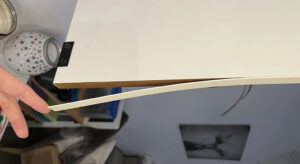
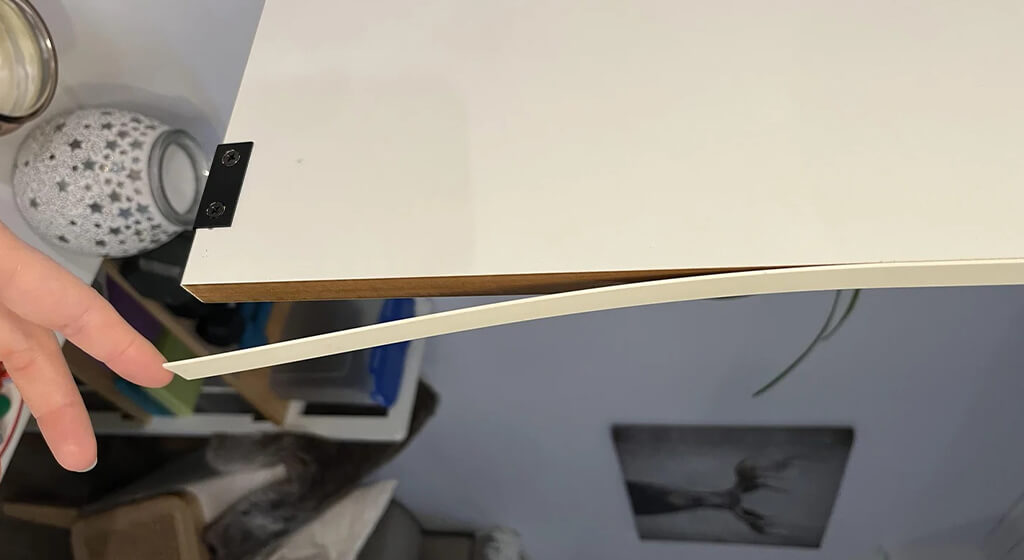
Edge banding peels off mainly because the adhesive fails to create a stable connection between the edge tape and the panel edge.
However, in real furniture production, glue is rarely the only reason. The final bonding quality depends on panel preparation, adhesive performance, pressing conditions, machine adjustment, and material compatibility.
After years of working with furniture factories and panel processing lines, we have found that many edge banding peeling problems are caused by small process issues that are overlooked during daily production.
The correct way to solve the problem is not to immediately change glue or increase temperature. It is to check the complete bonding process step by step.
Table of Contents
1. What Causes Edge Banding to Peel Off?
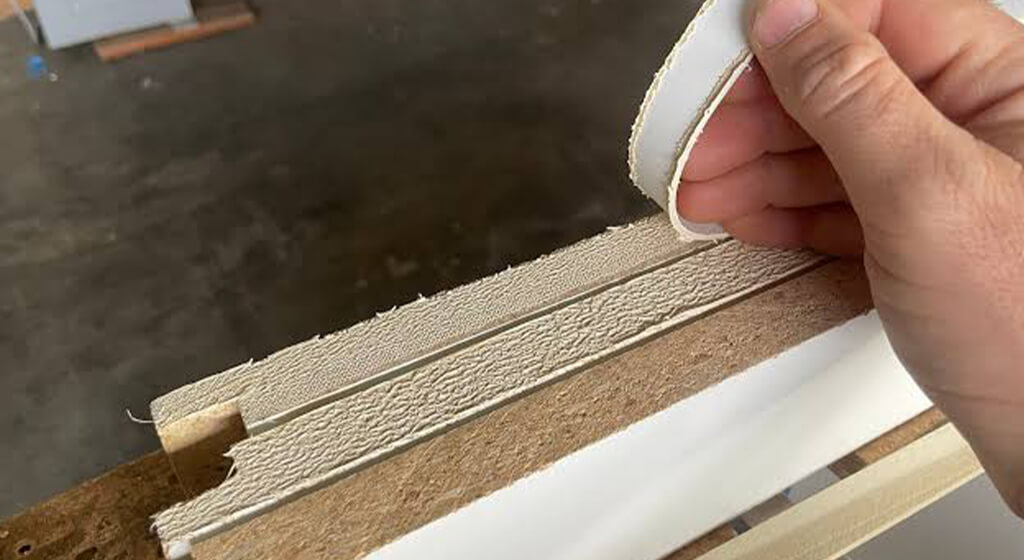
Edge banding failure is usually not caused by one single problem. It happens when one or more parts of the bonding process become unstable.
The complete edge banding process includes:
Panel edge preparation → Glue application → Edge tape pressing → Cooling → Final trimming and finishing
Each stage affects the final result.
For example, a factory may use high-quality adhesive but still experience peeling because dust remains on the panel edge. Another factory may have clean panels but poor bonding because the pressure rollers are not adjusted correctly.
When I troubleshoot an edge banding peeling problem in a factory, I usually check three basic questions:
- Is the panel edge clean and suitable for bonding?
- Is the adhesive applied under the correct conditions?
- Is the machine creating enough and stable pressure?
Bostik also said that successful bonding depends on selecting the correct adhesive system and applying it under suitable processing conditions. Both EVA and PUR hot melt adhesives are widely used in woodworking applications, but their characteristics and requirements are different.
Edge Banding Bonding Process and Common Failure Points
|
Process Stage |
What Happens |
Possible Failure Result |
|
Panel edge preparation |
The panel edge is cleaned and prepared for bonding |
Dust or damage can reduce adhesive contact |
|
Glue application |
Adhesive is applied to the panel or edge tape |
Incorrect glue amount can weaken bonding |
|
Edge tape pressing |
Rollers press the tape against the panel |
Poor pressure can create weak areas |
|
Cooling process |
Adhesive develops final strength |
Incorrect handling can affect stability |
|
Trimming and finishing |
Edge appearance is completed |
Wrong adjustment can damage the edge |
2. Cause 1: Dirty or Poorly Prepared Panel Edges
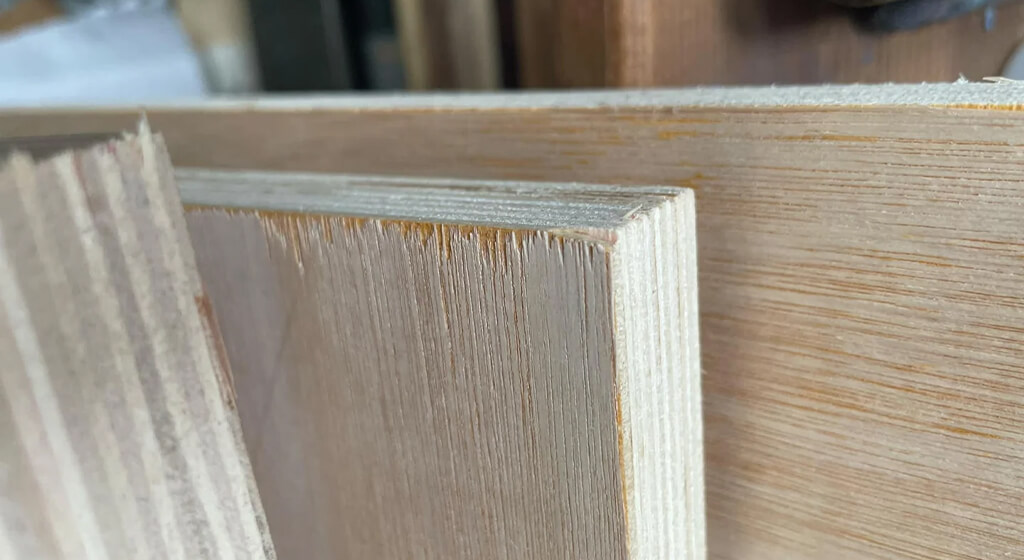
Edge banding requires a clean and stable panel edge because the adhesive needs direct contact with the board surface. If dust, loose fibers, moisture, oil, or damaged areas exist between the adhesive and the panel, the bond may become weak.
It is one of the most common causes of an edge banding peeling problem.
In many factories, operators first check the glue system when peeling occurs. However, the actual problem often starts before the panel reaches the edge banding machine.
2.2. Why It Happens
Panel edges can become contaminated during cutting, CNC machining, transportation, or storage.
MDF and particleboard are especially common sources of fine dust because their structure creates small particles during machining. These particles can remain on the edge surface even when the panel looks visually clean.
A rough or uneven edge can also reduce bonding quality. When the cutting tool becomes worn, the panel edge may have small damages or irregular areas. The adhesive cannot create the same contact condition as it would on a clean and uniform surface.
Another common issue is moisture. Panels stored in unsuitable conditions may absorb moisture, which can affect surface stability and bonding performance.
For high-gloss cabinet doors, even small edge preparation problems can become visible after production.
2.2. How to Fix It
Factories should improve panel preparation before edge banding by keeping cutting tools in good condition, removing dust from panel edges, and checking board quality before production.
For higher requirements, a pre-milling unit on an automatic edge banding machine can create a fresh and more consistent panel edge before glue application. This is especially useful for high-gloss panels, thin edge tape, and premium furniture production.
3. Cause 2: Incorrect Glue Temperature
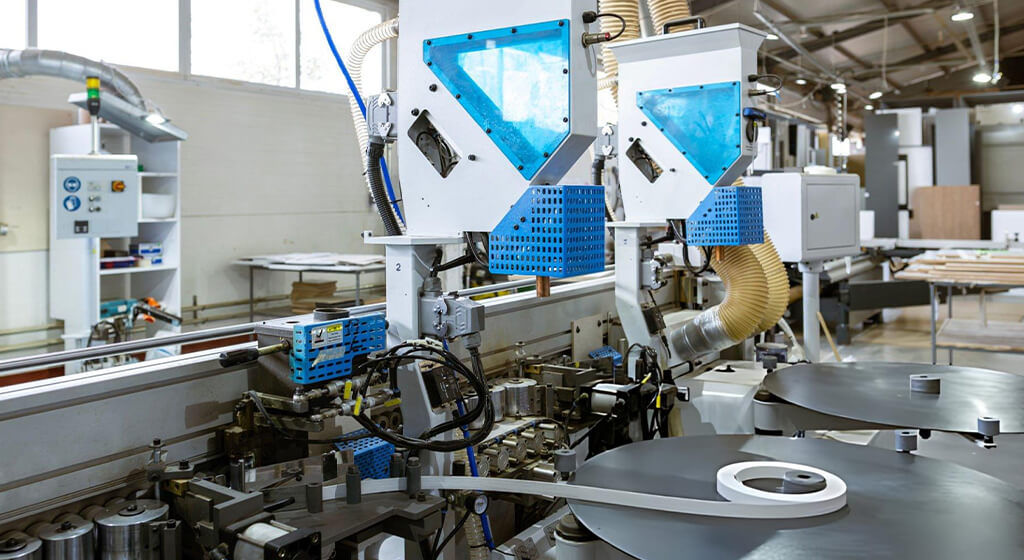
Glue temperature directly affects adhesive performance during edge banding.
The adhesive must reach the correct working condition before it can create a reliable connection between the edge tape and panel. If the temperature is too low or too high, the bonding process can become unstable.
3.1. Why It Happens
Glue temperature usually happen because the adhesive system is not adjusted according to the actual production conditions.
When the temperature is too low, the adhesive may not melt and flow correctly. The glue coverage can become uneven, and the contact between the tape and panel edge may not be strong enough.
When the temperature is too high, the adhesive may lose stable processing performance. The glue can become too fluid. It can create appearance problems, or reduced effectiveness over time.
Another common issue is insufficient warm-up time. Some factories start production before the glue pot reaches a stable working condition, which can create inconsistent bonding at the beginning of a production batch.
EVA and PUR edge banding systems also have different processing requirements. When selecting and operating adhesive systems, we need to consider the application and production environment rather than using one setting for every situation.
3.2. How to Fix It
Factories should follow adhesive supplier recommendations and maintain stable glue temperature during production.
Operators should allow enough heating time before starting work. We need check the adhesive condition regularly, and avoid changing temperature settings without understanding the real cause of the problem.
If edge banding starts peeling, temperature should be checked together with panel preparation, glue amount, and pressure adjustment.
It may make the better result by changing only the temperature, but may not solve the actual bonding problem.
4. Cause 3: Wrong Glue Amount
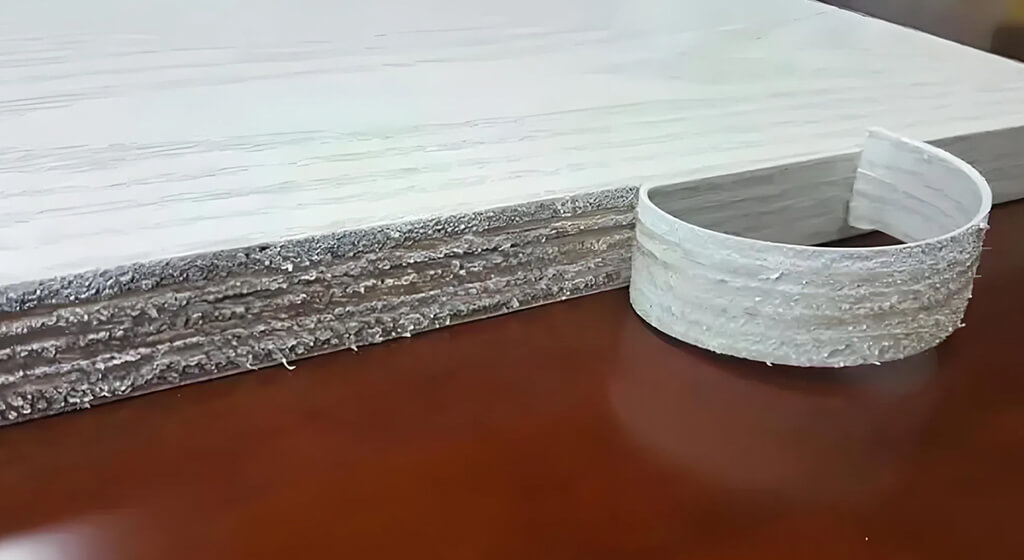
The correct glue amount is necessary for stable edge bonding.
A common misunderstanding in furniture factories is that more glue always means stronger bonding. In reality, excessive adhesive can create new problems, while insufficient adhesive can leave weak bonding areas.
The goal is to create a consistent adhesive layer between the edge tape and the panel, not the thickest possible glue line.
4.1. Why It Happens
Too much glue is usually caused by incorrect glue roller adjustment, unsuitable machine settings, or using the same glue amount for different edge materials.
Excessive glue can create visible glue lines, squeeze-out, longer cooling time, and additional cleaning work.
Too little glue creates another problem because the adhesive cannot cover enough surface area. The edge tape may appear attached after production but can separate later during transportation or customer use.
Production speed can also influence glue performance. When a factory increases machine speed without adjusting the adhesive application process, the glue layer may become inconsistent.
4.2. How to Fix It
Factories should adjust glue amount according to the edge tape material, panel condition, adhesive type, and machine speed.
Operators should check the glue roller condition, keep the glue system clean, and test sample panels before starting mass production.
A stable and controlled glue layer usually provides better bonding results than simply increasing adhesive volume.
5. Cause 4: Incorrect Pressure Roller Adjustment
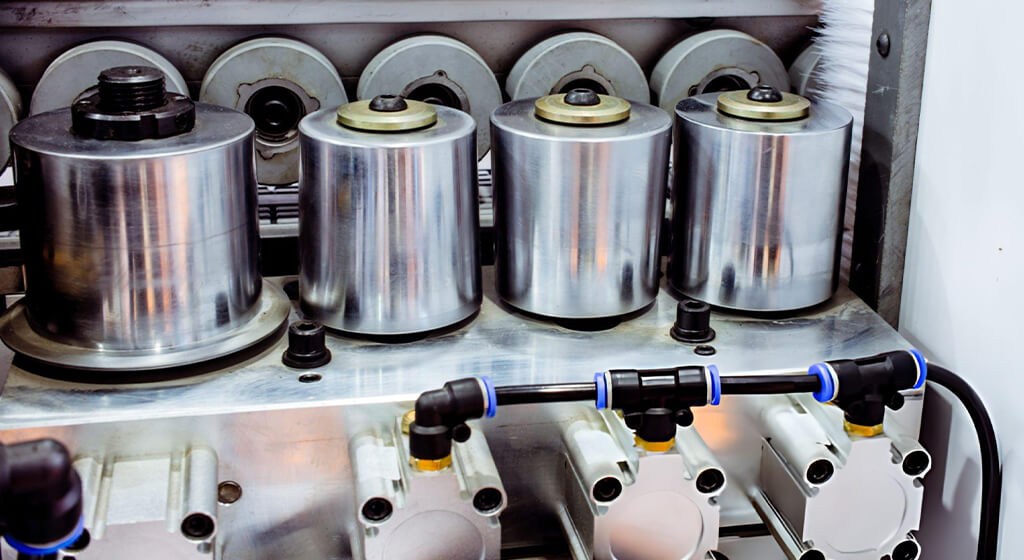
Pressure rollers play a critical role in creating a stable connection between the edge tape, adhesive layer, and panel edge.
Even when the adhesive type, temperature, and glue amount are correct, edge banding can still fail if the pressure system is not adjusted properly.
During the bonding process, the pressure rollers remove air gaps and help the edge tape fully contact the adhesive. If the contact is not consistent, weak bonding areas can appear.
5.1. Why It Happens
Pressure roller problems usually happen because the machine settings are not checked regularly or because adjustments change after maintenance.
When the pressure is too low, the edge tape may not fully contact the adhesive layer. Small gaps can remain between the tape and the panel, which reduces bonding strength.
When the pressure is too high, too much adhesive may be squeezed out from the bonding area. This can create a thin glue layer, uneven glue lines, and poor appearance.
Another common problem is uneven pressure across the panel. If one roller position is slightly different from another, one part of the edge may bond well while another part begins to peel.
In many factories, operators replace adhesive or increase glue volume when peeling occurs. However, after checking the equipment, the real problem is often a pressure adjustment issue.
5.2. How to Fix It
Factories should check pressure roller adjustment as part of regular machine maintenance.
Operators should confirm that:
- Rollers apply even pressure across the panel length.
- Roller positions match the edge tape thickness.
- Worn rollers are replaced when necessary.
- Machine settings are recorded after successful adjustment.
However, even advanced edge banding machine still requires correct setup and maintenance.
6. Cause 5: Wrong Adhesive (EVA vs PUR)
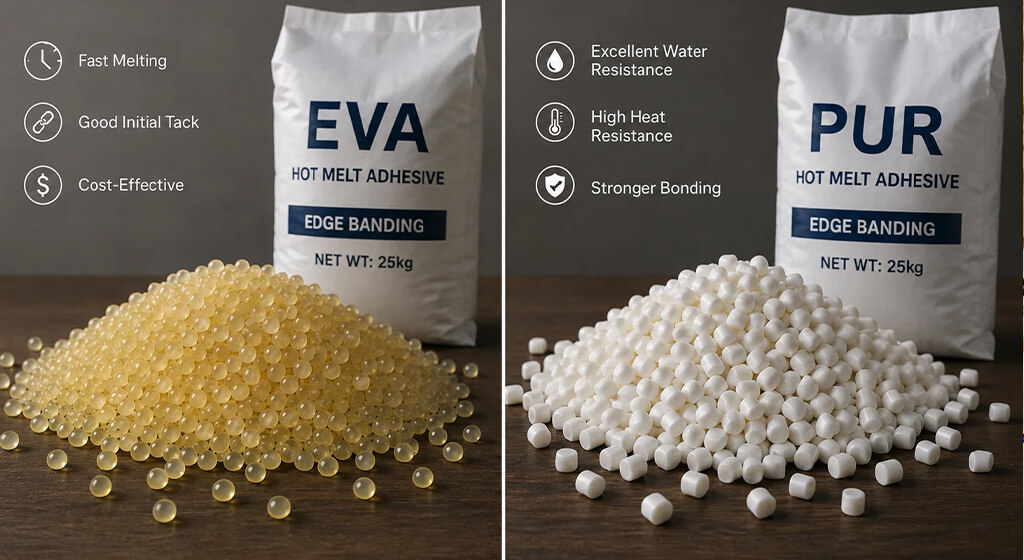
The correct adhesive is an important part of preventing edge banding adhesive failure.
Both EVA and PUR adhesives are widely used in woodworking applications. They have different bonding characteristics, processing requirements, and suitable applications.
Adhesive manufacturers such as Bostik provide both EVA and PUR glue for woodworking applications and explain that adhesive selection should consider the application, material, and production conditions.
6.1. Why It Happens
Some people choose glue based only on price or recommendations from other manufacturers. A solution that works well for one factory may not work for another because the production conditions are different.
For example, a bedroom furniture factory and kitchen cabinets facotry need a different glue.
Common selection mistakes include:
- Using standard EVA for products exposed to frequent moisture.
- Choosing PUR without having proper equipment and process control.
- Changing edge tape materials without testing adhesive compatibility.
- Selecting adhesive only because another factory uses the same type.
|
Feature |
EVA
Edge Banding |
PUR
Edge Banding |
|
Adhesive
type |
Thermoplastic
hot melt |
Reactive
polyurethane hot melt |
|
Processing
difficulty |
Easier
to operate |
Requires
more process control |
|
Cost |
Lower |
Higher |
|
Moisture
resistance |
Suitable
for standard applications |
Suitable
for demanding environments |
|
Glue
line appearance |
Good |
Very
thin glue line possible |
|
Common
application |
General
furniture production |
Premium
or moisture-sensitive products |
6.2. How to Fix It
Factories should select adhesive according to the final product instead of choosing based only on cost.
Before changing adhesive, manufacturers should evaluate:
- Where the furniture will be used.
- Whether moisture resistance is required.
- Which edge materials are being processed.
- Whether the production line supports the adhesive system.
The best adhesive is not always the most expensive one. It is the one that matches the application.
7. Cause 6: Incorrect Edge Tape Material
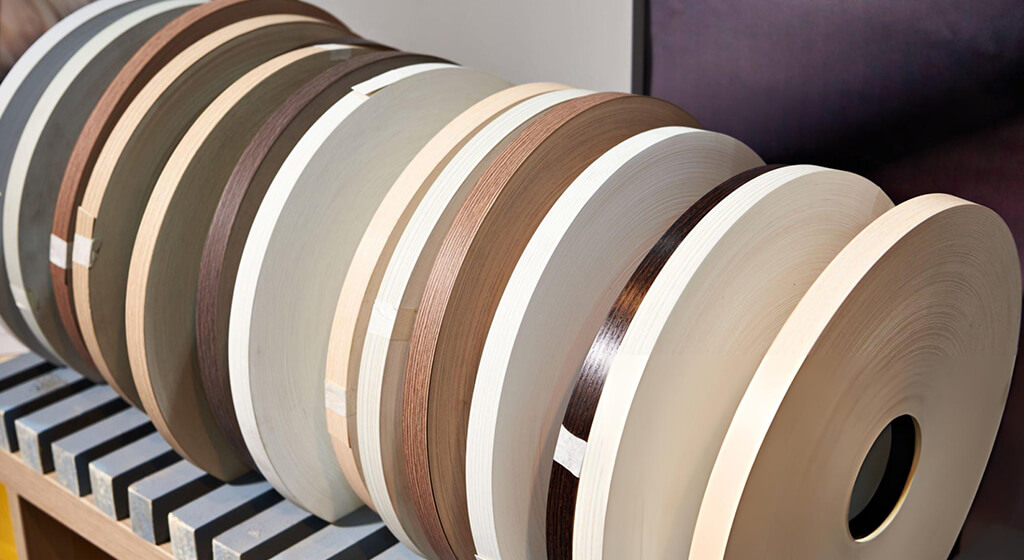
The edge tape and adhesive must work together to create a reliable bond. Even with correct machine settings, unsuitable edge material can cause peeling problems.
Common edge materials include:
- PVC
- ABS
- Acrylic
- Veneer
- Melamine edge banding
Each material has different surface characteristics, thickness, flexibility, and processing behavior.
7.1. Why It Happens
Edge tape problems usually occur when factories introduce new materials without adjusting the bonding process.
Different materials may require different adhesive conditions because their surfaces respond differently during heating and pressing.
For example, high-gloss acrylic edge materials have a very smooth appearance surface. Small bonding defects are easier to noted.
Veneer edge banding also behaves differently because it is a natural wood material. Changes in moisture and surface can affect processing stability.
Another common problem is changing edge tape thickness without updating machine parameters. A thicker or thinner edge tape may require different pressure and trimming settings.
7.2. How to Fix It
Factories should test new edge materials before full production.
A good preparation process includes:
- Checking adhesive compatibility.
- Testing sample panels.
- Adjusting machine parameters.
- Confirming edge tape thickness.
- Checking final appearance after bonding.
8. Cause 7: Machine Adjustment Problems
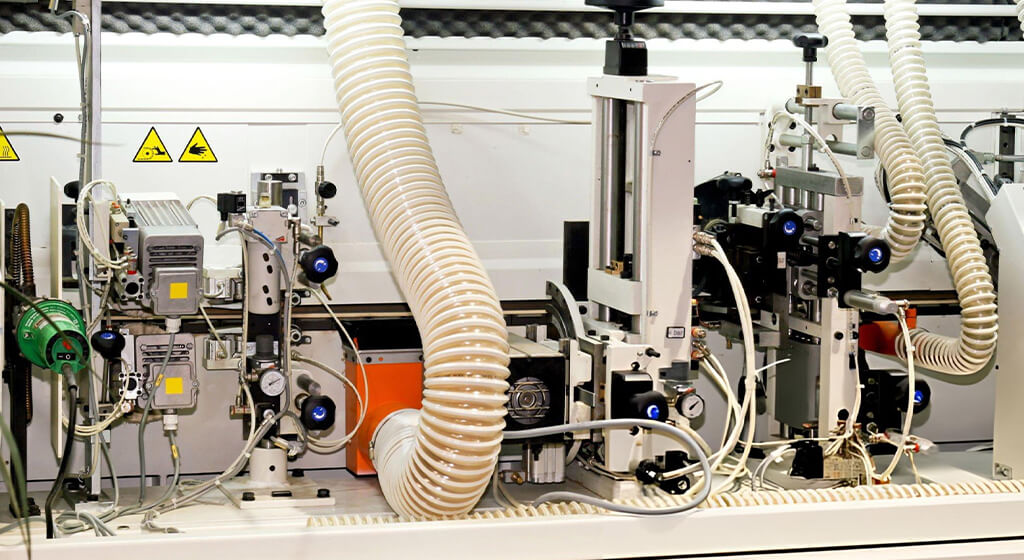
The woring machine set also caused edge banding peeling.
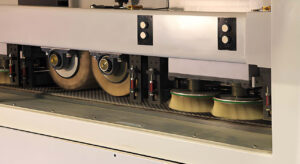
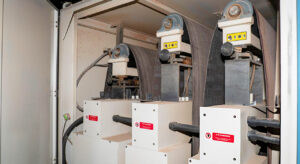
An edge banding machine is a complete processing system. The pre-milling unit, glue application system, pressure rollers, trimming units, scraping unit, and buffing unit all affect the final edge quality.
When one part is not adjusted correctly, the bonding result can become unstable.
8.1. Why It Happens
Machine adjustment problems usually appear after machine maintenance, operator changes, production speed changes, or new material introduction.
Common situations include:
- The pre-milling unit does not create a consistent panel edge.
- The pressure rollers are not adjusted according to edge tape thickness.
- The feeding speed is too high for the adhesive process.
- The trimming unit removes too much material.
- The scraping unit is incorrectly positioned.
- Polishing wheels become worn and affect the final appearance.
Another common issue is that operators use the same settings for different materials.
8.2. How to Fix It
Factories should treat machine adjustment as part of daily quality control.
Operators should:
- Record successful machine parameters for different materials.
- Check settings after maintenance.
- Inspect the first production pieces carefully.
- Replace worn tools on schedule.
- Train operators to understand the function of each unit.
For factories looking for stable edge banding machine troubleshooting, the first step should always be checking the complete process rather than changing only one parameter.
A well-adjusted machine reduces variation between operators and improves production consistency.
9. Cause 8: Environmental Conditions
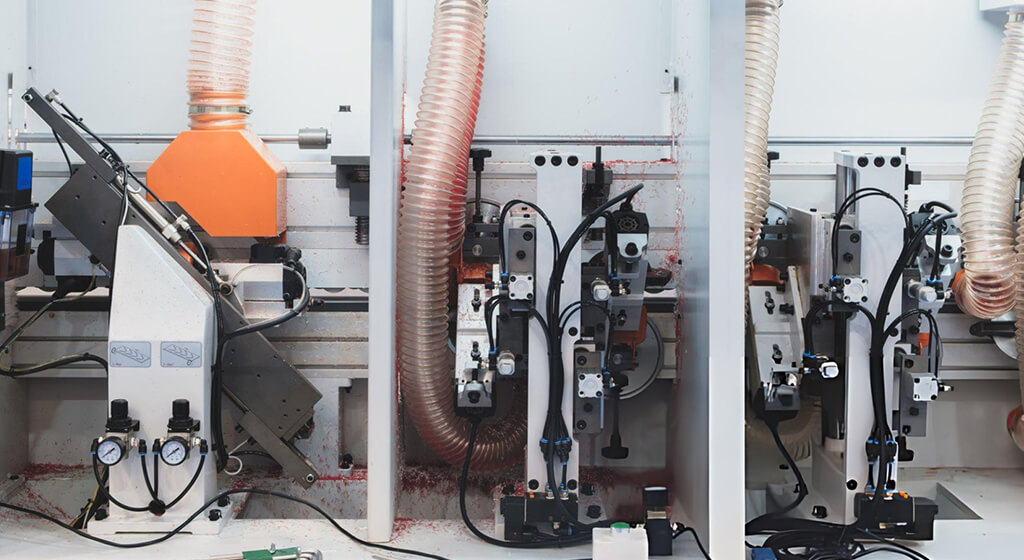
Environmental conditions can influence edge banding quality.
Furniture manufacturers often focus on machines and adhesives but overlook the condition of panels before processing.
Wood-based panels respond to changes in moisture and temperature. If the material condition changes, bonding stability can also change.
9.1. Why It Happen
Environmental usually make materials changing.
Common situations include:
- Panels stored in humid warehouses.
- Materials placed directly on concrete floors.
- Large temperature differences between storage and production areas.
- Edge tape stored in unsuitable conditions.
- Panels entering production immediately after transportation.
For example, a factory may receive panels during a rainy season and process them immediately without allowing the material condition to stabilize.
The machine settings may be correct, but the panel surface condition may have changed.
It can influence:
- Edge quality
- Adhesive contact
- Long-term bonding stability
Industry standards for wood products also recognize that material quality and stability are important factors in finished product performance. For example, ANSI/HPVA standards define quality requirements and testing considerations for hardwood and decorative plywood products.
9.2. How to Fix It
Factories should control material conditions before production.
Recommended practices include:
- Store panels in dry and stable areas.
- Protect materials from direct moisture.
- Allow panels to adapt before machining.
- Check incoming material quality.
- Avoid processing damaged or unstable boards.
Good edge banding quality starts before the panel enters the machine.
10. How to Improve Edge Banding Quality with the Right Machine?
For samll factories, manual adjustment may be manageable.
However, when production volume increases, machine stability becomes a key factor in maintaining consistent quality.
A good edge banding machine is not only increasing production speed. It can also create stable edge bonding and reduced rework.
10.1. Pre-Milling Unit
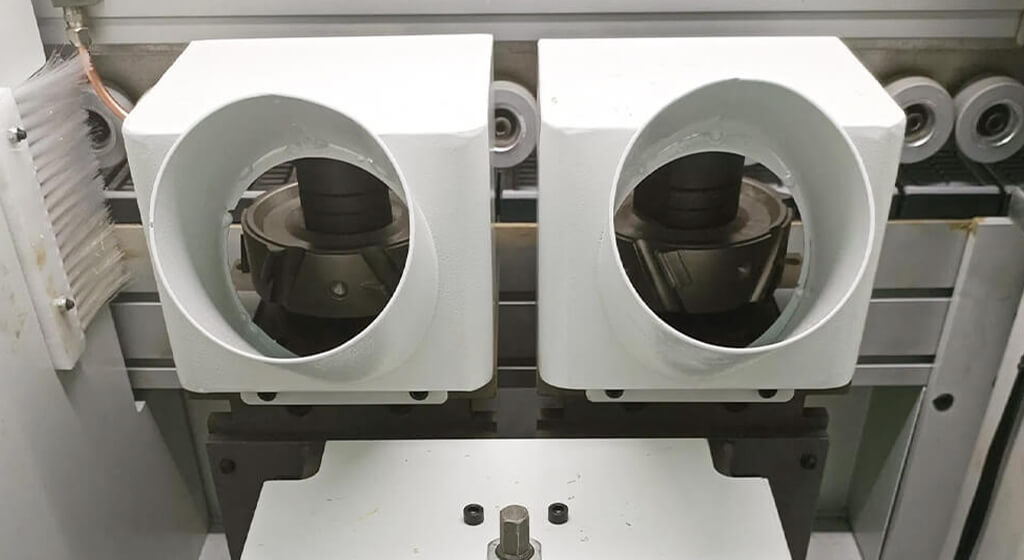
A pre-milling unit prepares the panel edge before adhesive application.
It removes a small amount of material to create a cleaner and more consistent surface.
This is especially useful for:
- High-gloss panels
- Thin edge tape
- Premium cabinet doors
- Large-volume production
A stable edge surface gives the adhesive better conditions for bonding.
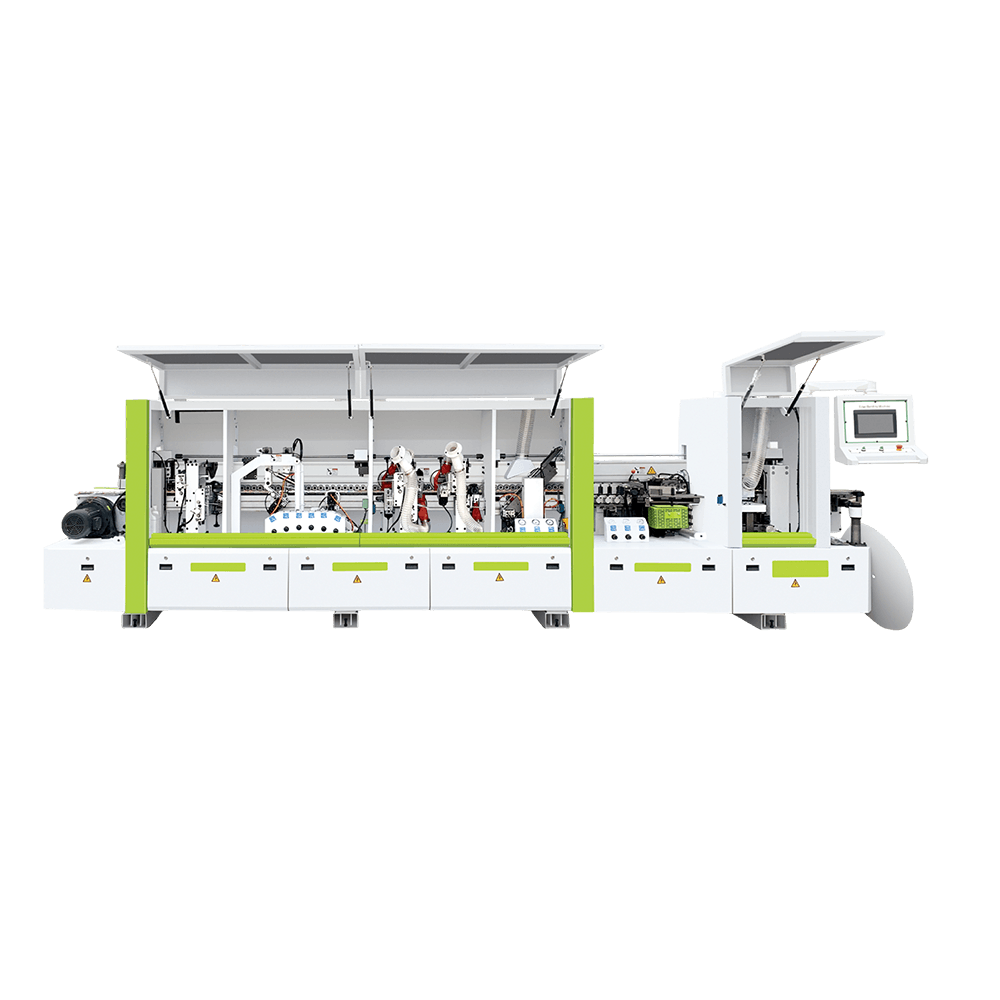
Straight Edge
F450DJ
- Pre-Mill —Glue —End Cut —Fine Trim —Corner Trim —Scrap —Flat Scrap—Buff
- EVA
- Edge Thickness: 0.4-3mm
- Panel Thickness: 10-60mm
- Size: 6800×950×1850mm
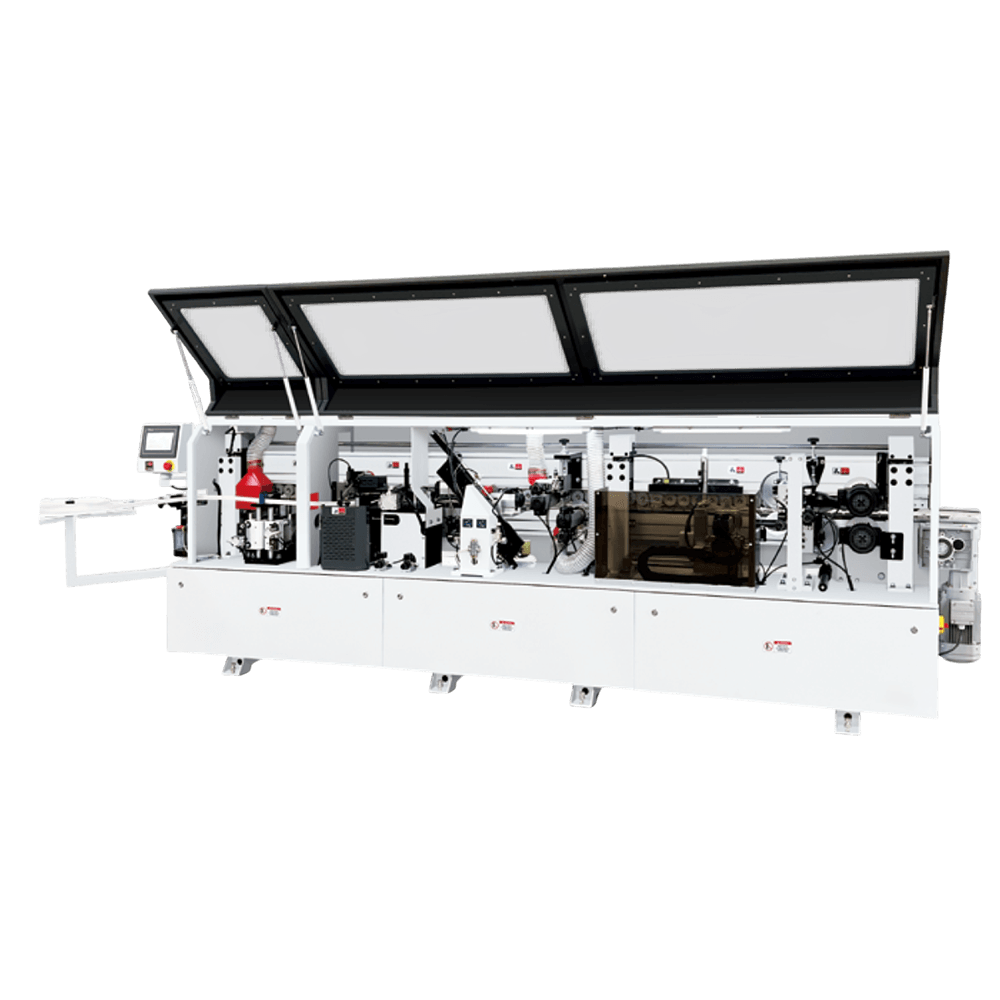
Straight Edge
F1
- Pre-Mill —Glue —End Cut —Rough Trim —Fine Trim —Corner Trim —Scrap —Buff
- EVA
- Edge Thickness: 0.4-3mm
- Panel Thickness: 10-45mm
- Size: 4250×600×1400mm
10.2. PUR Glue System
For products requiring improved resistance against moisture or demanding environments, a PUR glue system can be considered.
However, PUR is not automatically the correct solution for every factory.
The decision should depend on:
- Product application
- Customer requirements
- Production environment
- Operator capability
A factory producing standard office furniture may have different requirements from a manufacturer producing kitchen or bathroom cabinets.
10.3. Accurate Pressure Rollers
Stable pressure is essential for consistent bonding. A reliable pressure system helps maintain proper contact between:
- Edge tape
- Adhesive layer
- Panel edge
It reduces quality differences between operators and production shifts.
10.4. Scraping and Buffing Units
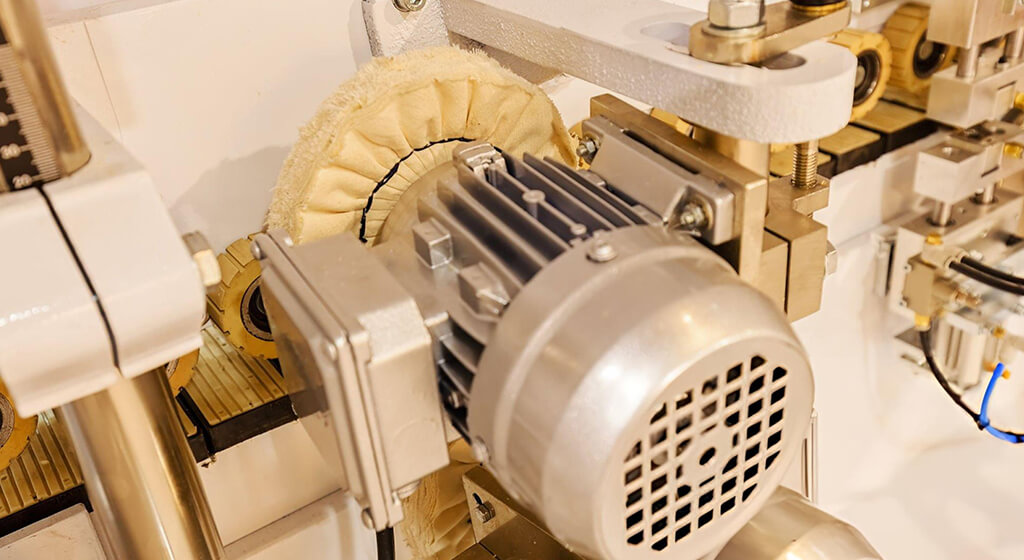
After bonding, finishing units improve the final appearance.
The scraping unit helps control glue line appearance.
The buffing unit improves the surface finish of decorative edge materials.
These units are especially valuable for furniture products where appearance quality is critical.
11. How to Improve Edge Banding Quality with the Right Machine?
To reduce edge banding failure, furniture manufacturers should focus on the complete production process instead of changing only one factor. Clean panel edges, suitable adhesives, correct machine settings, stable pressure, and proper material handling are the foundation of reliable edge bonding.
For factories producing large volumes of cabinet doors and panel furniture, machine stability and process strict control can significantly reduce rework and improve finished product quality.